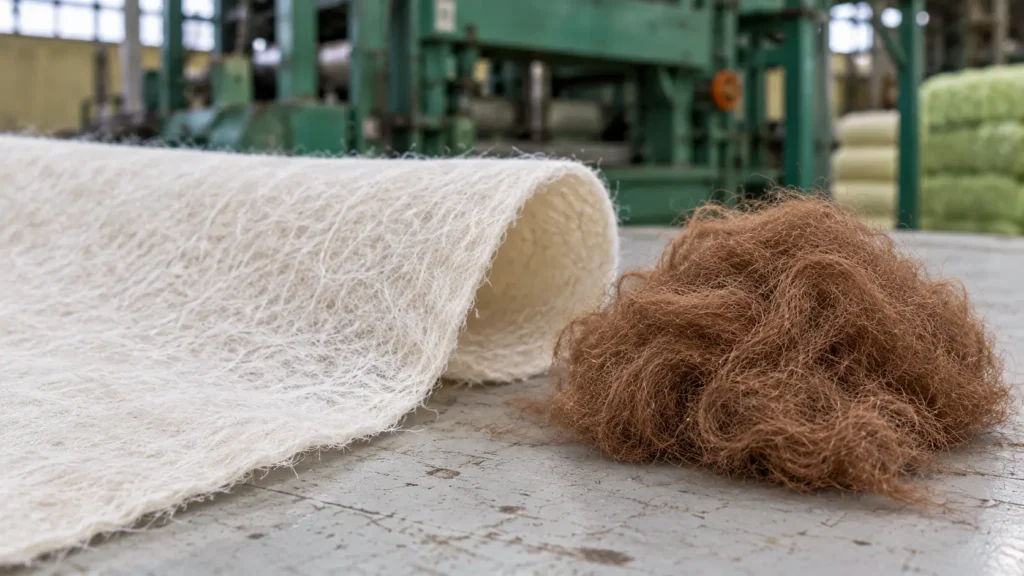
Choosing polyester staple fiber for nonwovens starts with your production process. First, identify how your line forms the fiber layer and bonds the fibers together. Then compare fiber grades against your equipment, product requirements and trial results.
A soft, clean sample may look suitable, but appearance alone does not show how it will perform during carding, needle punching or resin bonding. Base your purchase on its performance during production.
The Role of PSF in Nonwoven Structure
PSF means polyester staple fiber: short polyester fibers with a defined cut length. In a production line that uses staple fibers, equipment opens and blends the compressed fiber tufts before forming a layer.
Engineers call this initial fiber layer a “web.” The bonding stage gives the web the strength and stability that the finished product needs.
Carding helps separate, arrange and distribute fibers across the working width. Uneven feeding or fiber distribution can create thin areas, thick areas or fiber clumps. Later production stages cannot always correct these defects.
Alyaf Nemoune supplies solid polyester staple fiber in virgin and recycled grades. You can review the industries we serve to see where nonwovens fit within the company’s current applications.
Which Nonwoven Processes Can Use Solid Staple Fiber?
Nonwoven production includes several different processes. State your exact process when you discuss a fiber sample with a supplier.
| Process | Possible role of solid polyester staple fiber | What to check before ordering |
|---|---|---|
| Carding and needle punching | A fiber option for suitable felts and technical materials | Match fiber properties with the needles and machine settings |
| Web formation and resin bonding | A structural fiber component | Test surface finish compatibility with the binder and drying process |
| Web formation and thermal bonding | A structural component in a suitable blend | Identify which material provides the bonding function |
| Spunlace | An option that requires a specific technical review | Confirm the grade against the equipment and finished product requirements |
| Spunbond and meltblown | Ready made staple fiber does not normally serve as the direct feedstock | These processes form fibers directly from molten polymer |
During needle punching, special needles mechanically entangle the fibers. Needle selection, penetration depth and punch density also affect the result. Fiber quality alone does not determine product performance.
Some thermal bonding blends need binder fibers with a lower melting point. Alyaf Nemoune’s current product range does not include Low Melt fiber. For these blends, define the role of the solid polyester fiber separately from the bonding material.
Review Custom Grade Polyester Staple Fiber for the available specification options. Include your production process when you request a sample.
Choosing Denier and Cut Length for a Nonwoven Line
Denier describes fiber fineness, while cut length describes the length of each staple fiber. Choose both parameters around your equipment and the performance you need from the finished material.
Match Denier to the Finished Product
Before choosing denier, define your target basis weight, thickness, appearance and performance. Basis weight means the mass of one square meter of material, usually in grams per square meter.
For example, if surface uniformity matters, inspect fiber distribution and visible defects. If your product needs a certain bulk or mechanical strength, measure that property after bonding.
Lower denier does not automatically mean better quality. For a fuller explanation of the available options, read our polyester fiber denier guide.
Match Cut Length to the Equipment
Cut length must suit the opening equipment, card and fiber transport system. Your current fiber specification and the equipment manufacturer’s recommendations provide a useful starting point.
Record cut length during each trial. If you change length, denier and surface finish at the same time, you may find it difficult to identify which change affected the result.
Our guide to polyester fiber cut length and its effect on production explains this selection in more detail.
Compare Virgin and Recycled Grades Through Testing
The terms virgin and recycled describe the source of the raw material. They do not, on their own, predict how a fiber will perform on your line.
Check the grade specifications, cleanliness, batch consistency and trial results. Our virgin versus recycled polyester fiber comparison explains the broader selection criteria. For a nonwoven product, make the final decision using product quality and actual production cost.
Quality Parameters That Affect Web Uniformity
Web uniformity depends on both the raw material and the production line. Review fiber properties alongside feeding, opening, carding and web laying.
| Parameter | What to record |
|---|---|
| Denier and cut length consistency | How the sample matches the agreed specification and whether batches differ |
| Crimp | Fiber behavior during feeding, web formation and mechanical entanglement |
| Surface finish | Fiber movement, static buildup and compatibility with the bonding process |
| Cleanliness and opening | Foreign particles, dust, fused fibers and fiber knots |
| Fiber distribution | Differences in basis weight, thickness and appearance across and along the web |
Do not judge surface finish only by touching a sample. A more slippery finish can change fiber movement, but you also need to assess its effect on fiber entanglement or bonding.
If the web has thin and thick bands, check feeding and distribution across the working width. If you see clumps or knots, inspect fiber opening and card settings as well. A visible defect does not prove its cause.
Evaluate the web and the finished product separately. If the web looks uniform but the finished material lacks strength, investigate the bonding stage and its settings too.
A Checklist for Testing Samples on Your Line
The following trial plan gives purchasing, production and quality teams a shared basis for comparing samples.
1. Set Acceptance Criteria Before the Trial
Define the required basis weight, thickness, appearance and performance. Depending on the application, you may also need to measure tensile strength in both production directions, air permeability or thickness recovery after compression.
Choose a test method and an acceptable limit for each property. Descriptions such as “softer” or “better” do not provide enough detail for an industrial purchase decision.
2. Record the Sample and Line Conditions
Write down the sample code, batch number, denier, cut length, surface finish and blend ratio. Also record line speed, main machine settings, environmental conditions and trial time.
Keep a reference sample of the incoming fiber and the finished material. These samples give your team a clear comparison point for future deliveries.
3. Separate the Initial Comparison From Line Adjustment
First, compare the new sample with your current fiber under comparable conditions, within the equipment’s operating limits. This stage helps reveal differences in material behavior.
Next, adjust the line where necessary for the new sample and record each change. This stage shows what the material can achieve with suitable settings.
4. Take Samples Across the Width and Over Time
Once the line runs steadily, take samples from several positions across the web and at different times. Do not approve a grade based on one good looking section.
Measure basis weight and thickness with a consistent method. Test the finished product against its application requirements, and record results before and after bonding separately.
5. Compare Waste and Downtime Alongside Quality
Record waste, production stops, cleaning needs and the line speed you can maintain. The price per kilogram of fiber represents only part of the purchase cost.
For a practical material cost comparison, divide the cost of the raw material consumed by the quantity of saleable product. This calculation includes the effect of material loss.
6. Put the Approved Specification Into the Order
After your team approves a sample, include its grade code, technical specification and acceptance limits in the order. Agree with the supplier on the documents that will accompany the material.
A Technical Data Sheet, or TDS, describes the product specification. A Certificate of Analysis, or COA, gives batch test results. Before ordering, confirm which properties and test methods the supplier will include.
Frequently Asked Questions
Is Every Solid Polyester Fiber Suitable for Nonwovens?
No. The production process, equipment, grade specification and finished product requirements determine suitability. Approval on one line does not guarantee the same result on another.
Which Denier Should I Choose for Needle Punched Felt?
There is no single denier for every felt. Review basis weight, thickness, required performance, needle selection and equipment before testing a proposed grade.
Should I Change the Fiber If the Web Is Uneven?
First, identify where the defect starts. Unstable feeding, poor opening, card settings and web laying can also affect uniformity. Then compare the alternative fiber under recorded conditions.
Is Siliconized Fiber Always Better for Nonwovens?
No. Siliconization changes the surface properties of the fiber. Its value depends on the process and product. Test fiber movement and bonding performance with an actual sample.
Request a Sample for Your Nonwoven Line
Prepare your product name, production process, equipment details, target basis weight and current fiber specification. Describe any problems, such as knots, uneven basis weight or excessive waste.
Then request a polyester fiber sample for your nonwoven line through our contact page. Add these details to the Inquiry Details field.
If you do not know the required denier or cut length, explain your line conditions and target result. The Alyaf Nemoune team can help identify suitable options for a trial.
Sources
- EDANA: How Are Nonwovens Made? explains web formation, bonding methods and the differences between processes that use staple fibers and molten polymer.
- Trützschler: Nonwoven Carding Technologies explains how opening, blending and fiber distribution affect web quality.
- Groz Beckert: Staple Fiber Needle Punch Line describes a technical trial line for fiber preparation, carding and needle punching.
- Groz Beckert: Nonwoven Needling Parameters explains the importance of needle selection, penetration depth and punch density.